11 workshops, one roof
Stamping, laser cutting, CNC bending, welding, polishing and assembly all run in-house, so tolerances are held from the first blank to the final finish.
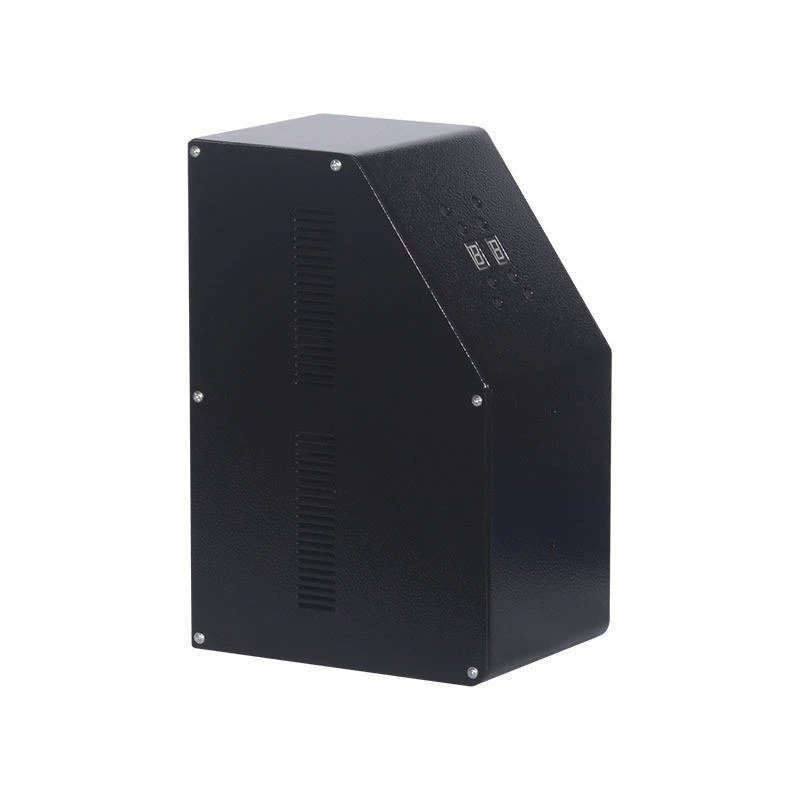
Main photo: production sample. More angles and a video are available on request.
cnc aluminium equipment enclosure · Equipment Enclosure
Aluminium equipment enclosure machined from plate, with matching brackets and panels.
ISO 9000 (quality management system) and CCC held. Inspection records ship with every batch, and third-party inspection is welcome before loading. How we document a shipment
Overview
Tooling, stamping, laser cutting, bending, welding and surface finishing all run in our eleven workshops in Foshan — the part never leaves the plant between steps.
When an enclosure needs a thick boss, a pocket for a heat spreader or a face that stays flat across its whole length, forming alone will not get there. This build starts from aluminium plate and machines the features that a bent sheet cannot hold.
The body is milled, drilled and tapped, then the matching brackets and panels are cut and formed from sheet so the assembly still closes on a gasket. Deburring is done by hand on the machined edges, and the finish is applied with the earth points and the sealing faces masked.
Send the assembly model and say which faces are datum. We decide what is machined and what is formed, quote both, and keep the two processes in one production file so the parts meet at assembly.
This part runs at 10 pcs per batch, with the die designed and maintained in our own tool shop. If you need a smaller trial before committing to the run, say so in the enquiry and we will quote the two quantities side by side.
Specifications
Values below describe our standard process window for this product line. Tighter tolerances and other alloys are quoted case by case.
| Material | Aluminium, with stainless brackets where needed |
|---|---|
| External size | Custom, up to 4,500 mm |
| Wall thickness | Machined from plate; thickness to your drawing |
| Machining | Milled pockets, bosses, tapped holes and sealing faces |
| Matching parts | Brackets and panels cut and formed from sheet |
| Finish | Anodised or powder coated, with masked earth and seal faces |
| Inspection | Critical dimensions measured against the model |
| Drawing files | PDF, DWG, DXF, STEP or a physical sample |
| MOQ | 10 pcs |
| Lead time | 4 to 7 working days after drawing approval |
Send a drawing for a part-specific data sheet.
Why this drawing matters. Every tolerance, hole position and bend radius on this page is confirmed against a drawing during quotation — so what you approve is what gets inspected at the end of the line. The published drawing is a generic sample, never a customer's file.
These are applied for by the importer in its own market — that is the normal division of labour in this trade. What we do is supply the samples, material data and process records your test house asks for, and manufacture and inspect to whichever standard your drawing names (ASTM, EN, ISO). What we will not do is put a mark on a part we have not tested.
Why this part
Every one of them sits inside our own plant, on the same floor as the parts.
Stamping, laser cutting, CNC bending, welding, polishing and assembly all run in-house, so tolerances are held from the first blank to the final finish.
160T × 2, 100T × 4, 80T × 8 and 60T × 12 presses, plus a 350T hydraulic press for deep-drawn housings and larger shells.
This part is produced in batches of 10 pcs. Tooling is built here, so the die stays with the part and a repeat order does not pay for it twice.
Three utility patents on our own tooling. The die is built and maintained by the same team that runs the press, so a design change moves with the part.
ISO 9000 and CCC held. Each batch leaves with an inspection record, material certificates on request, and third-party inspection is welcome before loading.
SGS, TÜV, BV or your own QC team can walk the line and inspect finished parts at our plant. Reports go to you, not to us.
Production process
Five steps, in this order, all in Foshan.
Send a PDF, DWG, DXF or STEP file. We check material, sheet thickness, tolerance and surface finish, and flag anything that needs adjusting before quoting.
Dies are designed, cut and maintained in our own tool shop — three utility patents on our tooling. A design change moves with the part.
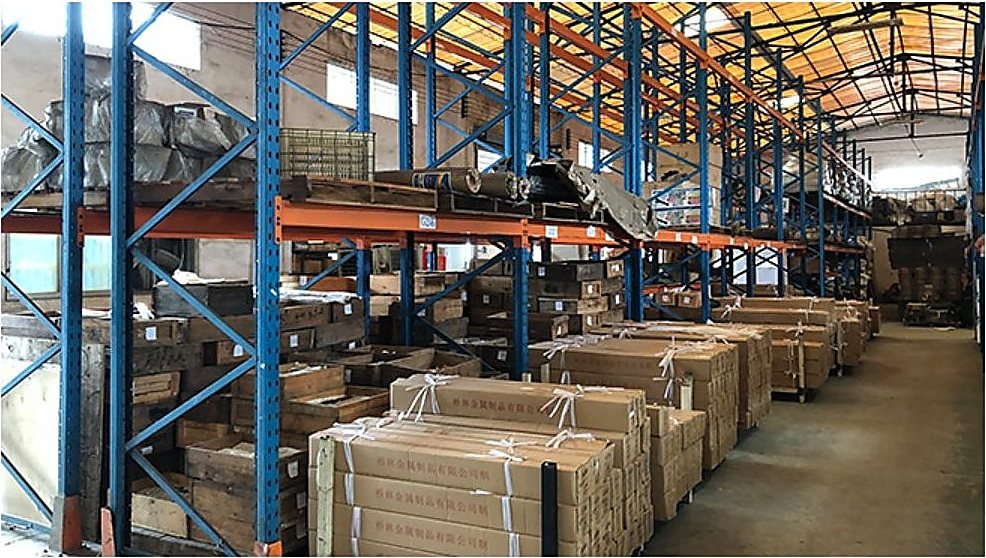
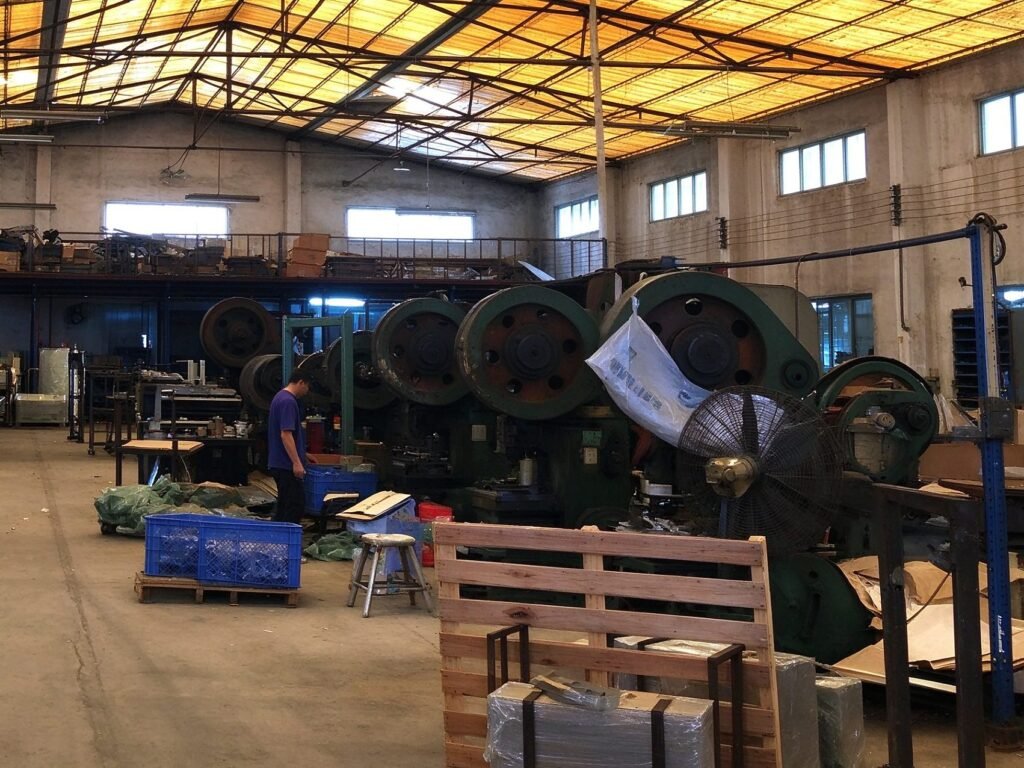
26 presses from 60T to 160T, plus a 350T hydraulic press for deep-drawn shells. Laser cutting and CNC bending handle blanks and complex forms.
Tapping, welding, grinding and polishing complete the part. Surface treatment is specified to your drawing and documented per batch.
Incoming checks, in-process checks and a final layout inspection. SGS, TÜV, BV or your own QC team are welcome before loading.
Factory
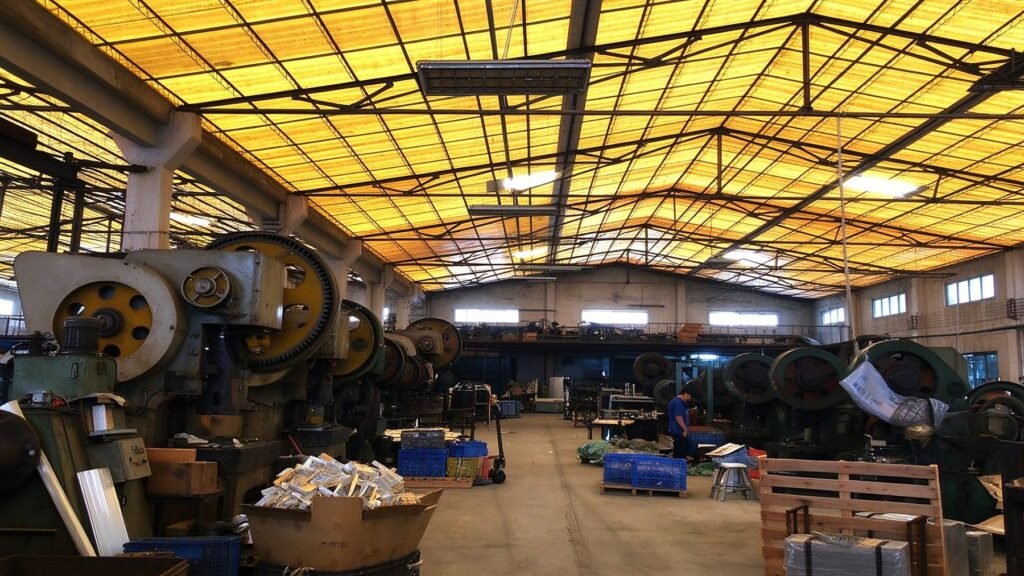
We run 13,000+ m² across eleven workshops in Foshan, Guangdong, China, with 51–100 staff. Sheet metal is the whole plant: the die is built where the part is stamped, the finish is applied where the part is formed, and a quality question is answered by the people who made the part.
How to order
Four steps, no account required. We reply within one working day.
PDF, DWG, STEP files or a physical sample all work. Tell us the quantity you have in mind — one piece is a valid starting point.
We confirm material, tolerance and surface finish, and flag anything that needs adjustment before quoting.
A prototype is produced in 4-7 days so you can verify fit, finish and assembly before committing to volume.
Laser cutting, CNC bending, punching, welding and in-house surface treatment are all completed under one roof for consistent quality.
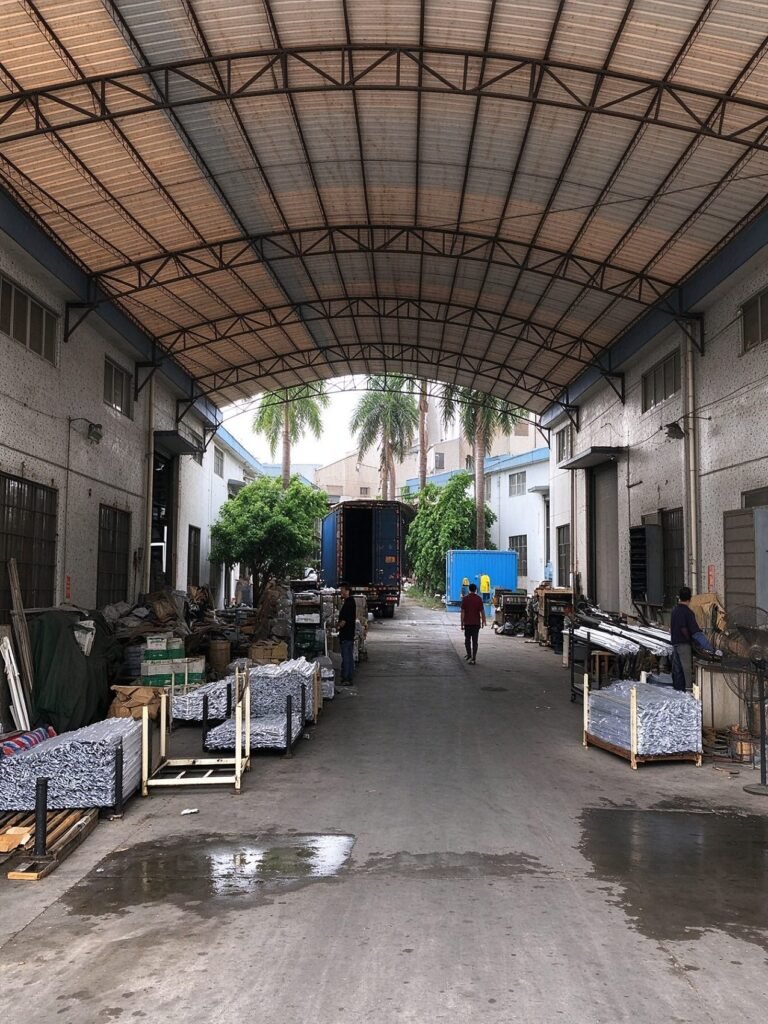
OEM and ODM projects are welcome, and we can support you in meeting your target-market certification requirements. Cnc aluminium equipment enclosure are produced in our Foshan factory, where 26 punch presses plus CNC laser cutting and bending equipment handle both one-off prototypes and repeat production runs.
FAQ
The questions buyers ask most before requesting a quote.
Related products


Request a quote
Tell us the part, material, dimensions and quantity. PDF, DWG, DXF, STEP files or a physical sample all work. If your enquiry needs an engineer's input we tell you the expected date instead of leaving you waiting.
Prefer to talk?
WhatsApp / Phone +86 18588672899
gdtokin@gmail.com